Introduction — a familiar morning at the plant
I remember walking into a production line where cartons were piling up at the end of a conveyor like toys after a birthday party — messy and stressful. In that moment an automatic case packer sat idle (belt stopped), costing the team minutes of lost throughput and a cascade of manual fixes. Data from that shift showed cycle time drift and nearly 12% downtime across a week; the numbers hit you in the gut. So I asked myself: what small checks could have prevented that sticky morning — and how do you pick a machine that won’t make you repeat it? Let’s unpack this step by step, with practical notes you can use tomorrow.
Deeper issues with current solutions
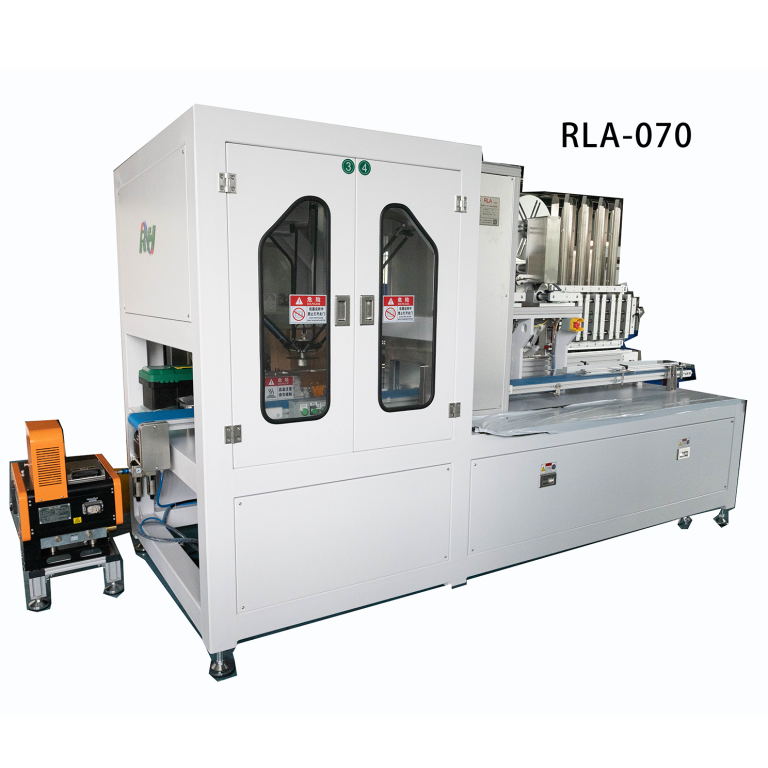
automatic case packer manufacturers often ship machines that look great on paper but strain under real shifts — I’ve seen it. The first flaw is hidden rigidity: a machine tuned to one SKU can’t adapt to size changes without long downtime. The second is control mismatch. Poor PLC setup and poorly matched servo motors cause jerky motion and misfeeds. Third, systems lack modern inspection: without a decent vision system small sealing errors go undetected until the pallet is already on the dock.
Why do these systems fail so often?
Technically speaking, conveyors aren’t the enemy — integration is. When conveyor integration is an afterthought, synchronization fails. You end up fighting stack alignment and sensor noise, and then maintenance becomes reactive. Look, it’s simpler than you think: if the control architecture (PLC, HMI) and motion hardware (servo motors, drives) aren’t designed as a coherent system, you pay in scrap and frustrated operators. I’ve watched teams spend days tweaking parameters only to uncover a missed wiring harness or a misconfigured encoder — funny how that works, right?
New technology principles that actually matter
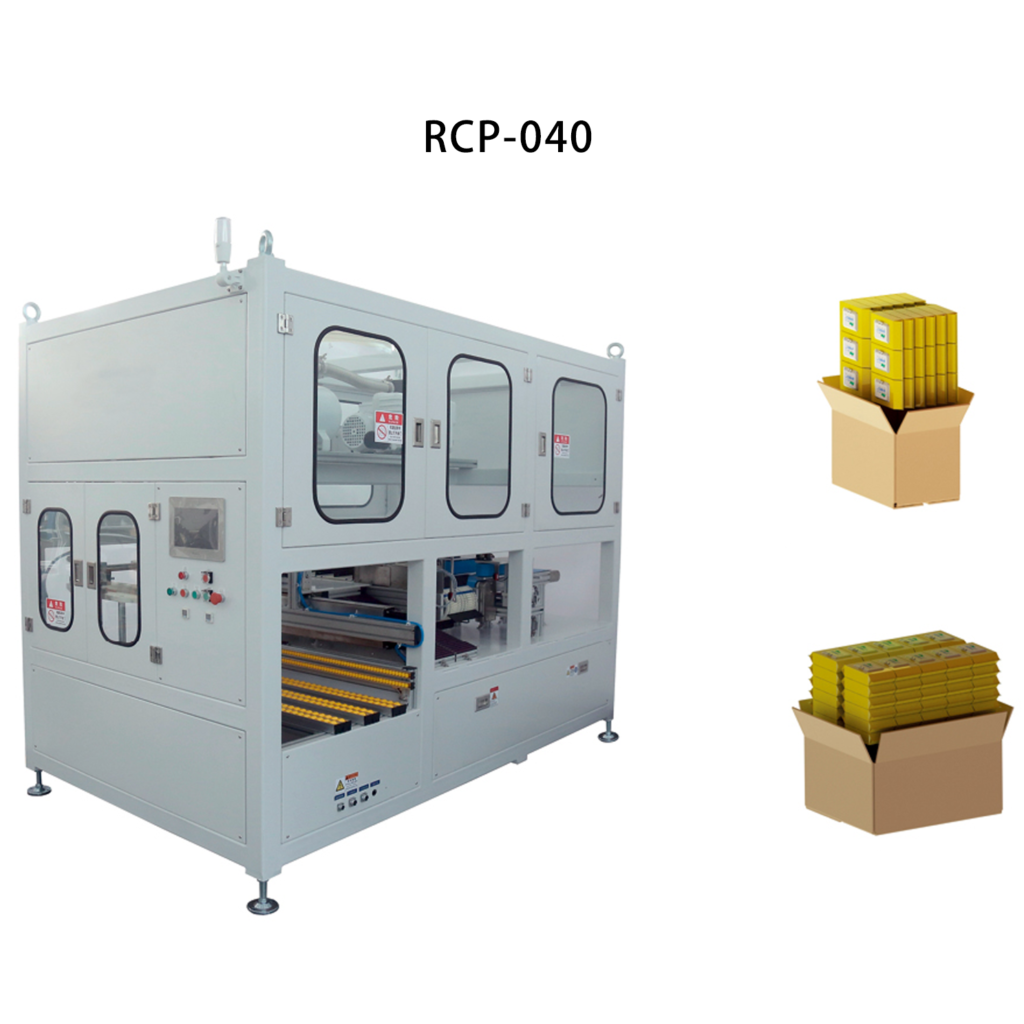
What I want to see now — and what I recommend you ask for — are machines built around modular control and smarter sensing. That means edge computing nodes that handle local decision-making, vision systems that validate case fill before sealing, and power converters sized to support peak torque without sag. When vendors (yes, even automatic case packer manufacturers) design with modular I/O and open protocols, integration with existing MES or SCADA becomes less painful. I prefer semi-formal demos: short, real-case runs with my SKU list — not generic cycles.
What’s next for buyers?
Going forward, demand systems with predictive maintenance hooks and easy access points for technicians. Ask for clear documentation on how the HMI displays alarms, how firmware updates are applied, and whether spare parts are standardized. — and yes, that matters. Compare suppliers on three hard metrics: throughput under mixed SKUs, mean time to repair (MTTR) with a novice technician, and total cost of ownership over five years. Weigh those numbers, visit a live line if you can, and don’t sign off until a short acceptance run uses your actual cartons.
Final takeaways and three evaluation metrics
In short: I want practicality over polish. Machines should be flexible, maintainable, and honest about limits. From my experience, the best upgrades reduce operator interventions and make troubleshooting straightforward. Here are three metrics I use when evaluating options — keep them front and center when you talk to suppliers:
1) Throughput consistency: measure real throughput across your full SKU mix, not just the fastest case. 2) Maintainability (MTTR): how quickly can a line tech get the machine back running with basic tools? 3) Integration friction (TCO impact): quantify the time and cost to connect to your PLC/MES and any recurring service fees.
We’ve learned that the right questions uncover the right machines. If you approach suppliers with these checks, you’ll cut the “surprise days” on the line. For hands-on help and reliable options, I recommend starting conversations with trusted partners like ZLINK — they’ll show you real runs, not just glossy brochures. 54 ARTICAL
When Lines Breathe: A Comparative Look at Flexibility in Wholesale Wet Wipe Production
Introduction — A Small Factory Moment, Big Numbers, One Question
I once watched a morning shift where the worker paused, cupped a fresh wipe, and smiled—simple, human. In that pause I thought of scale: a single machine in a modest plant can make thousands of units per hour, and a full wholesale wet wipe production line often targets tens of thousands daily (these are not empty claims; the order books show it). So where does real value lie—speed, cost, or the kind of flexibility that saves a plant from stoppages and customer complaints?
I write as someone who has walked factory floors and argued with engineers; my tone is both careful and a little lyrical—amar mone hoy we must balance poetry with pragmatism. I will sketch problems and hopes in plain language, drop in a few technical terms like PLC and servo motor, and keep the view close to the workers and managers who live this work. Let us move to the heart of packaging and its hidden frictions—so we can see what to fix next.
Part 1 — The Hidden Flaws of Wet Wipe Packaging (Technical)**
wet wipe packaging looks tidy in brochures. I’ll be blunt: on the line it can be messy. Machines sing a steady hum—servo motors drive film unwind, PLCs orchestrate timing—but small mismatches multiply. A flawed reel stand or bad roller tension control can skew the web. Ultrasonic sealing that is slightly off will make packs leak. Vision inspection catches some defects, but not all. Look, it’s simpler than you think: a tiny misfeed costs hundreds of rejected packs an hour.
We often focus on throughput and neglect the human cost. Operators juggle cutter assembly jams, adhesive misses, and sticky wipes that cling to guides. The spare parts supply chain lags. Power converters trip during heat spikes. Meanwhile, clients demand consistent barcodes and tamper-evident seals. I have seen quality teams work late nights to rework pallets—stressful, inefficient. The problem is not a single defect, but the system’s brittle response to everyday variation. That brittleness shows most where packaging intersects with change: product formulas, tissue weight, fragrance loads. These are not exotic failures; they are the daily grind of wet wipe packaging (and yes—funny how that works, right?).
Where do these breakdowns start?
Usually at an interface: a sensor mismatch, a speed mismatch between dosing pumps and cutter, or a poorly calibrated ultrasonic head. Small misalignments cascade. I’ve learned that diagnosing these requires both shop-floor empathy and tools like oscilloscopes, PLC logs, and spare-part inventories.
Part 2 — New Principles and a Forward-Looking View
Now I shift forward. I want to outline technological principles that can make packaging resilient. First, modular design. I prefer machines built as replaceable modules—reel stand, dosing station, sealing head, vision unit. It lets us swap a failing cutter assembly without halting the whole line. Second, closed-loop control. Use sensors plus PLC logic to adjust roller tension in real time. Third, smart diagnostics. Edge computing nodes can host simple anomaly detection close to the machine, so faults are flagged before they grow (this reduces downtime and keeps morale intact).
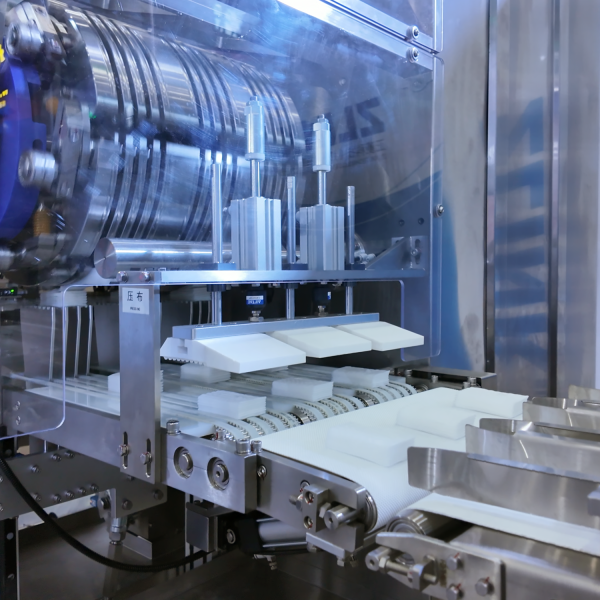
Let me give a short case example: a mid-size plant I worked with replaced a fixed-speed feeder with a servo-driven, feedback-controlled feeder. The result: fewer misfeeds, less scrap, and a 12% rise in effective throughput. They added a vision inspection camera at the packer and linked it to PLC alarms. Now an operator gets an on-screen prompt, not a loud buzzer—calmer shop floor, faster responses. These changes are not magic. They are engineering choices—servo motor upgrades, robust power converters, and smarter human-machine interfaces. They matter for wet wipe packaging and the bottom line. — and yes, we saved on overtime too.
Real-world Impact?
In practice, modularity and diagnostics shorten mean time to repair. They also let teams run mixed SKUs with less manual changeover. I believe this is where flexibility shows its value: not only in higher output, but in lower stress, fewer reworks, and better customer trust.
Conclusion — Lessons, Metrics, and a Humble Look Ahead
I’ll be straightforward: I favor flexibility because I’ve seen it rescue plants from market swings and supplier hiccups. If you ask me to recommend a path, I offer three practical metrics you can use to evaluate systems: mean time to repair (MTTR), scrap rate per million units, and changeover time between SKUs. Measure these quarterly and aim for steady improvement. Don’t chase flashy specs; invest in good PLC programming, reliable ultrasonic sealing heads, and a modest vision system that actually gets used by operators.
We must keep the human element central. Operators are not cogs—they are the system’s senses. Train them, listen to their fixes, and incorporate their tweaks into design updates. I’ve watched simple operator suggestions cut a daily downtime by hours—small ideas, large savings. If you want a partner who understands both the poetry and the nuts-and-bolts of this work, start with practical steps: modularity, feedback control, and on-line diagnostics. That’s my candid counsel.
I mention this with no hype—just conviction. For solid, field-proven lines and support, consider the solutions and engineering I’ve seen in action at ZLINK. They helped a plant I know move from brittle to durable, and that mattered to me, and to the people who run those lines every day.